Antifouling, Hull Coatings & Marine Painting in West Papua
Blasting, primer, antifouling and topside painting for vessels in Sorong and Raja Ampat. Coating systems specified for high-fouling tropical water, applied and recorded.
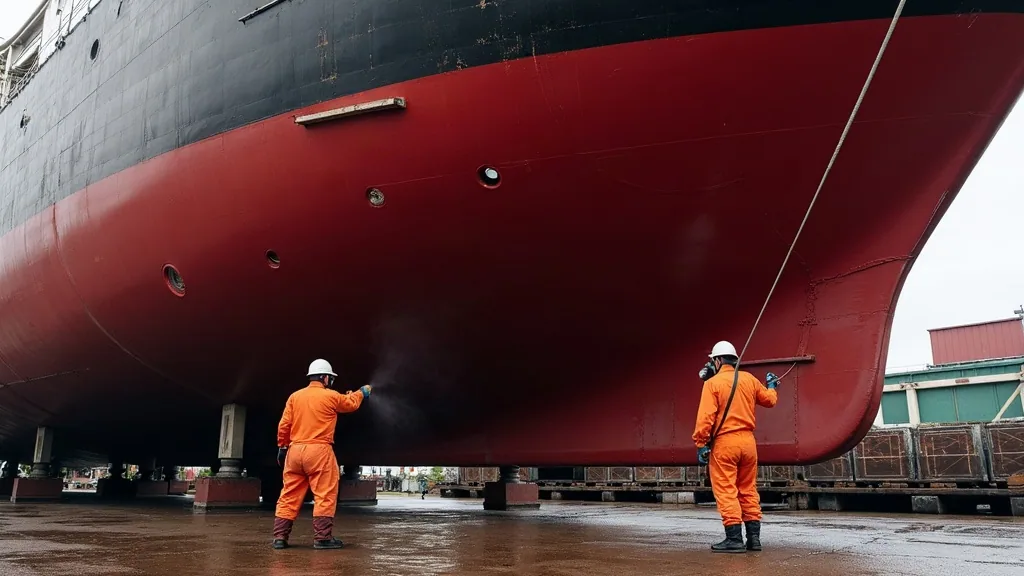

Raja Ampat is one of the most aggressive fouling environments in Indonesia — warm, nutrient-rich
water and vessels that spend long periods at anchor. Antifouling here is a specification problem before it is a
painting problem. We select a coating system against the vessel’s actual duty cycle, prepare the substrate properly, apply to
the manufacturer’s film thickness, and record what went on so the next docking starts from fact.
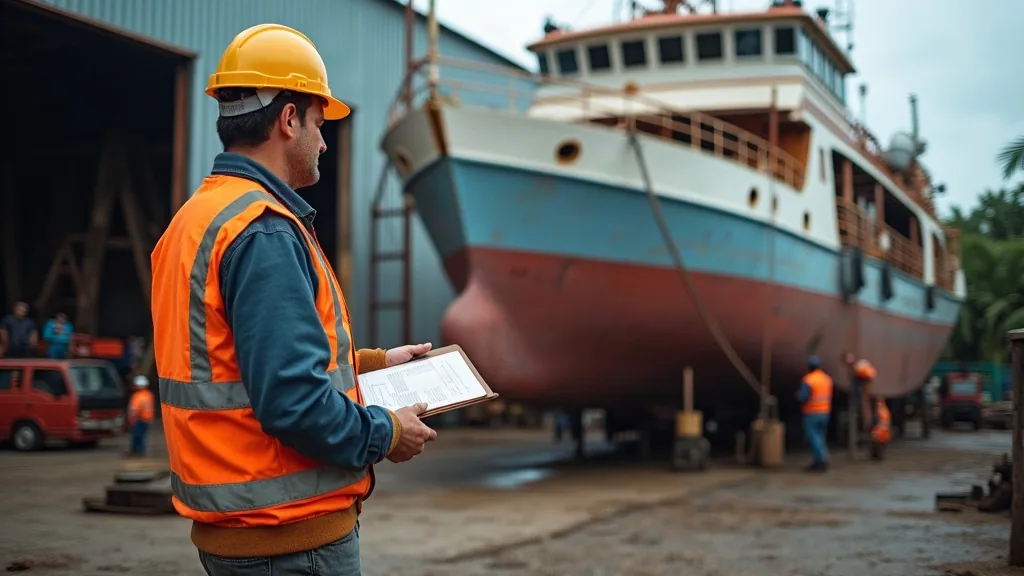
Why paint fails early in this region
Three causes account for most of the premature failures we are asked to fix:
- Wrong product for the duty cycle. Self-polishing copolymer antifoulings rely on water movement to renew
their surface. A dive liveaboard that sits at anchor for eighteen hours a day and moves at eight knots between sites is not
polishing that film. Hard-matrix or high-copper-content systems, or a hybrid, usually outperform an SPC on this fleet. - Preparation shortcuts. Painting over a failing previous scheme, over residual salt, or over a surface that
was pressure-washed but never dried gives a coating that lifts in sheets in nine months, regardless of what it cost. - Film thickness by eye. Two thin coats look identical to three correct ones on the day of launch. They are
not identical eighteen months later, and without wet-film readings there is no way to prove which one you paid for.
The scope we work to
- Condition assessment — adhesion testing on the existing scheme, identification of the incumbent product
family, and a decision on whether to overcoat or strip. Overcoating an unknown or incompatible system is the most common
avoidable mistake in this region. - Preparation — high-pressure fresh-water wash immediately after lift while growth is still soft, then
mechanical sanding, sweep blasting or full blast to bare substrate depending on the assessment. Steel is prepared to an agreed
surface standard, and blasting waste is contained rather than left on the foreshore. - Priming and barrier coats — anticorrosive on steel, epoxy barrier on GRP where osmosis history or moisture
readings justify it, and appropriate primers on wooden hulls tied into the
caulking and sheathing programme. - Antifouling — two or three coats to specified dry film thickness, with a contrasting signal coat so the
next crew can see when they are through to primer. - Boot-top and topsides — polyurethane or acrylic finish, with fairing where the hull warrants it.
- Records — batch numbers, ambient and substrate temperature, humidity, dew point margin, wet and dry film
readings, and photographs at each stage.
How long antifouling actually lasts here
For a working dive liveaboard in Raja Ampat waters, a correctly specified and correctly applied system generally gives
usable protection for twelve to eighteen months, with some hard-matrix schemes reaching around twenty-four months on vessels
that move more and anchor less. Vessels that sit for extended periods, or that carry a compromised previous scheme, will foul
faster no matter what is applied. The variables that move that number most are duty cycle, anchoring time, water temperature at
the operating sites, and whether the hull is cleaned in the water between dockings.
In-water cleaning between dockings extends the interval but has to be done gently — an aggressive scrub on a soft SPC film
removes the biocide reservoir and shortens the life of the scheme. We would rather clean three times lightly than once
hard.

Coating work as part of a docking
Coatings are almost never the reason a vessel is lifted, but they are usually the reason it stays on the hard longer than
planned. Blasting cannot start until structural work in that area is finished, paint cannot go on a wet or contaminated
surface, and cure schedules are fixed by the product and the weather. So the coating programme is planned backwards from the
launch date at the same time as the docking window is booked, and any
hull repair is sequenced to clear the areas the painters need
first.

Anodes and corrosion protection
Coating and cathodic protection are one system, not two. Every docking includes an anode audit: wastage assessment on the
existing anodes, a check that bonding straps are continuous and clean, calculation of the required anode mass for the interval
until the next lift, and correct positioning — including shaft, rudder and internal sea-chest anodes that are routinely
forgotten. Persistent, unexplained anode consumption is usually an electrical problem rather than a paint problem, and it gets
referred to the electrical desk rather than absorbed with
more zinc.
What you receive
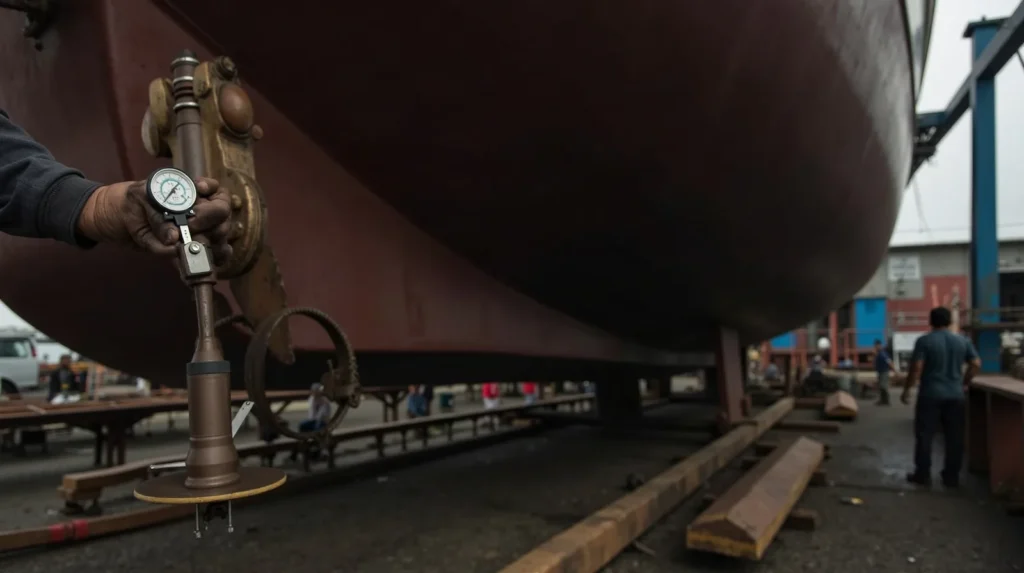
A coating report with the product data sheets, the actual conditions on the days of application, film thickness readings and
photographs. It is a short document and it is the reason your next paint decision can be made on evidence. Budget shapes for
coating cycles across a five-year maintenance plan sit on the
refit budgeting page.
Talk to the repair desk
Send the vessel particulars — length overall, beam, draft, hull material, displacement, current location and the window you have available — and the Raja Ampat Shipyard Desk will come back with a written scope and a quotation in USD for coatings and antifouling. Quotations name the yard, the slipway or dock, the work sequence and the assumptions behind every line.
WhatsApp: +6281139414563
Email: bd@juaraholding.com
Contracts for construction, repair, refit and vessel-sale work are issued by PT Komodo Galangan Nusantara. All quotations are stated in USD.
Further reading from the field notes
Frequently asked questions
How long does antifouling last in Raja Ampat waters?
Twelve to eighteen months is the realistic planning figure for a working liveaboard, and some hard-matrix systems reach around twenty-four months on vessels that move regularly. Long periods at anchor, warm nutrient-rich water and any compromise in surface preparation all pull that number down.
Can you overcoat my existing antifouling?
Only after adhesion testing and identification of the incumbent system. If the existing scheme is failing or incompatible, overcoating buys a few months and then fails in sheets, taking the new paint with it. We will tell you which case you are in before quoting.
Do you clean hulls in the water between dockings?
Yes, and for most Raja Ampat operators it is worth doing. It has to be gentle: aggressive scrubbing strips the biocide from a self-polishing film and shortens the life of the scheme. Light, frequent cleaning outperforms one hard clean.
How do I know the paint was applied to the right thickness?
Wet film readings during application and dry film readings afterwards, recorded against the product data sheet requirement, with batch numbers and ambient conditions. Those readings are part of the handover file.